SPIRAX SARCO · CONDENSATE MANAGEMENT SYSTEMS
Spirax Sarco CCD Condensate Contamination Detection System
Spirax Sarco CCD system monitors condensate conductivity and diverts contaminated water to drain. Ideal for boiler protection in Indian factories.
Overview
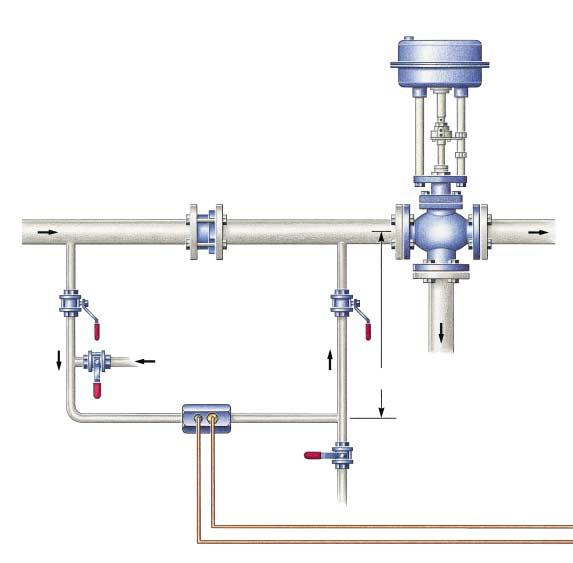
The Spirax Sarco CCD (Condensate Contamination Detection) system is an automatic monitoring solution designed to protect boiler systems from contaminated condensate return. By continuously measuring the conductivity of condensate, the system detects contamination and diverts affected condensate to drain before it can enter the boiler feedtank.
Returning clean condensate to the boiler house is essential for energy efficiency, reduced water treatment costs, and lower make-up water consumption. However, even low levels of contamination can cause foaming, scaling, or corrosion in the boiler, leading to costly downtime and product quality issues. The CCD system provides continuous protection by automatically isolating contaminated condensate while allowing clean condensate to return normally.
The system uses a robust high-temperature conductivity sensor with integrated temperature compensation, ensuring accurate readings regardless of condensate temperature fluctuations. When conductivity exceeds the pre-set threshold, a 3-port diverter valve (or dual 2-port valve arrangement) redirects contaminated condensate to waste, resuming normal operation once conductivity returns to acceptable levels.
Key Features
- Continuous real-time conductivity monitoring of condensate return lines
- Automatic diversion of contaminated condensate to drain
- Pt100 temperature compensation sensor for accurate readings across varying temperatures
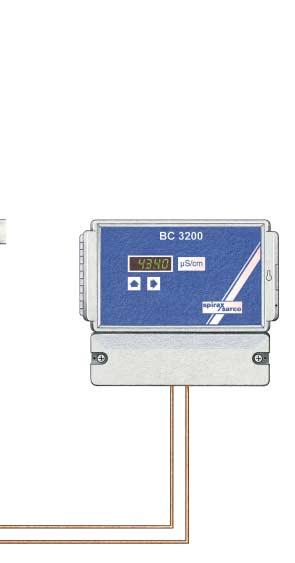
- Choice of wall-mounted (BC3200) or panel-mounted (BC3210) controllers
- 4-digit LED/LCD display with simple push-button commissioning and calibration
- Dual relay outputs for diverter valve control and alarm activation
- 0/4-20 mA analogue output for integration with plant control systems
- IP65 protection rating on controller for industrial environments
Specifications
| Parameter | Value |
|---|---|
| Nominal Conductivity Range (Normal) | 0–100 µS/cm (ppm) |
| Nominal Conductivity Range (Extended) | 0–1,000 µS/cm or 0–10,000 µS/cm |
| Supply Voltage | 230 V / 115 V |
| Supply Frequency | 50–60 Hz |
| Maximum Ambient Temperature | 55°C |
| Controller Protection Rating | IP65 |
| Sensor Chamber Connection | 1¼" BSP |
| Sample Connection | ¼" BSP |
| Controller Models | BC3200 (wall-mounted), BC3210 (panel-mounted) |
| Sensors Included | CP10 conductivity sensor, TP20 temperature sensor |
Applications
The Spirax Sarco CCD system is suitable for any industrial facility where condensate is returned to the boiler feedtank:
- Process industries: Chemical plants, pharmaceutical manufacturing, food and beverage processing - Textile mills: Dyeing and finishing operations with steam-heated equipment - Paper and pulp plants: Steam systems with multiple heat exchangers - Refineries and petrochemical plants: Critical boiler water quality requirements - General manufacturing: Any facility with indirect steam heating where product contamination of condensate is possible
The system is particularly valuable where condensate may become contaminated by process fluids through heat exchanger tube failures or leaking coils.
Product Images
Frequently Asked Questions
Get a Quote
Contact PC Engineering for pricing, availability, and technical support for the Spirax Sarco CCD Condensate Contamination Detection System. Call us or fill in our inquiry form — our engineers will respond within 24 hours.
More from Spirax Sarco
- Spirax Sarco CP42 Twin Tip Conductivity Probe for Boiler TDS Control
- Spirax Sarco CVS10 Sanitary Check Valve – ASME BPE Compliant for Pharma & High Purity Applications
- Spirax Sarco DCV10 & DCV10C Centrally Guided Disc Check Valves – Stainless Steel & Carbon Steel
- Spirax Sarco DCV3 Disc Check Valve – Stainless Steel Wafer Pattern Check Valve (IBR Certified)
- Spirax Sarco DCV4 Stainless Steel Disc Check Valve – IBR Certified Wafer Pattern
- Spirax Sarco DCV41 Food+ Austenitic Stainless Steel Disc Check Valve
Brand
Find the losses before you invest in new equipment.
Steam and pump system walkthroughs that identify inefficiencies, energy losses and improvement priorities before any new product is specified.